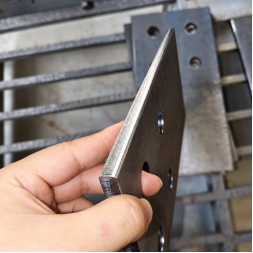
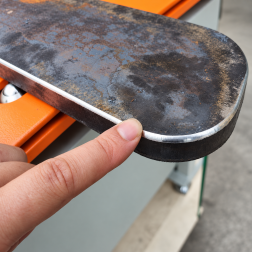
Fabricators often ask whether removing a burr is the same as producing a controlled radius. It is not. Deburring removes unwanted projections, while edge rounding changes the geometry to a specified R or C profile. The GCM-R3T Deburring and Chamfering Machine uses a guided milling head and carbide inserts to create repeatable paint-ready edges on steel plates and profiles, reducing dependence on variable hand grinding.
How Deburring and Edge Rounding Differ
| Requirement | Deburring Result | Chamfering or Rounding Result | Buyer Acceptance Point |
|---|---|---|---|
| Geometry | Removes loose or raised burrs | Creates a defined C or R profile | State R2, R3, C2 or C3. |
| Consistency | May only break the sharp edge | Controls edge shape along the length | Inspect radius and continuity. |
| Coating preparation | Eliminates projections | Improves coating wrap at the edge | Confirm paint-ready finish. |
| Production control | Manual result varies by operator | Guided milling supports repeatability | Approve a sample on actual material. |
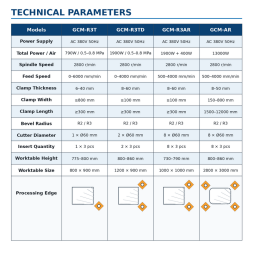
GCM R3T Technical Parameters
| Product Page | Power Supply | Total Power | Spindle Speed | Feed Speed | Plate Thickness | Edge Profiles |
|---|---|---|---|---|---|---|
| GCM-R3T Rounding | AC 380 V 50 Hz | 790 W | 2800 r/min | 0-6000 mm/min | 6-40 mm | R2 / R3 / C profiles |
| GCM-R3T Chamfering | Same model | Same specification | Same specification | Same specification | Same specification | Same machine different color |
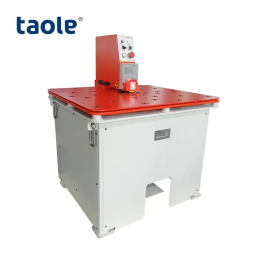
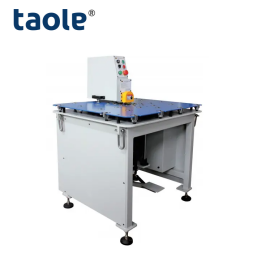
Product Links:
https://www.bevellingmachines.com/gcm-r3t-rounding-machine.html
https://www.bevellingmachines.com/gcm-r3t-metal-edge-rim-chamfering-machine.html
Both links describe the same GCM-R3T platform in different colors. The stationary system combines adjustable feeding with a single milling head and three carbide inserts. At up to 6000 mm/min feed and 2800 r/min spindle speed, the metal edge rounding machine is intended for repeatable processing of carbon steel, stainless steel, aluminum and alloy-steel workpieces rather than uncontrolled freehand removal.
The business case is strongest where parts require a defined radius before coating. Sharp corners can leave thin paint coverage and are difficult to reproduce by manual grinding. A controlled paint-ready edge improves process consistency, operator safety and inspection traceability. However, a radius machine is not automatically a heavy slag remover: buyers processing plasma-cut dross should describe the incoming edge condition and confirm whether a separate slag removal machine is needed before rounding.
Important Procurement Note:
The official page shows two different minimum-width figures: at least 80 mm in the summary and at least 800 mm in the parameter table. Procurement teams should therefore confirm minimum width, workpiece support and the required R/C tooling in the signed technical agreement before placing an order.
Buyer FAQs
| Procurement Question | Short Answer |
|---|---|
| Can GCM-R3T deburr and round an edge? | Yes, for controlled edge breaking and R/C profiles; submit the incoming burr condition for confirmation. |
| Are the two linked machines different models? | No. Both pages describe GCM-R3T; the visible machine color differs. |
| What should buyers send for a quote? | Provide material, thickness, minimum width and length, edge profile, burr or slag condition and output target. |
Post time: Oct-26-2026